

 Cr15Al5
 Cr19Al3
 Cr25Al5
 Cr23Al5Ti
 Cr21Al16Nb
 Cr27Al7Mo2
 Cr20Ni80
 Cr30Ni70
 Cr15Ni60
 Inconel 625
 Inconel 718
 Inconel 725
 Inconel X-750
 Inconel 690
 Inconel 617
 Inconel 601
 Inconel 600
 Inconel 686
 Inconel 602CA
 Incoloy A-286
 Incoloy 825
 Incoloy 925
 Incoloy 926
 Incoloy 800
 Incoloy 800H
 Incoloy 800HT
 Incoloy 909
 Incoloy 31
 Incoloy 901
 Monel K-500
 Monel 400
 Nimonic 263
 Nimonic 75
 Nimonic 80A
 Nimonic 90
 Nimonic PE11
 Nimonic PE16
 Nimonic PK33
 Nimonic 901
 Nimonic 81
 Nimonic 86
 Nimonic 105
 Nimonic 115
 Hastelloy C-276
 Hastelloy C
 Hastelloy C4
 Hastelloy C-22
 Hastelloy C-2000
 Hastelloy B-2
 Hastelloy B-3
 Hastelloy G30
 Hastelloy X
 Super Invar 32-5(4J32)
 Alloy 36(4J36)
 Alloy 42(4J42)
 Alloy 50(1J50)
 Hiperco 50(1J22)
 Alloy 46
 Permalloy (1J79)
 Supermalloy(1J85)
 ERNiCrMo-2
 ERNiCrMo-3
 ERNiCrMo-4
 ERNiCrFe-7
 ERNiCrFe-7A
 ERNiCrMo-10
 ERNiCrCoMo-1
 ERNiFeCr-2
 ERNiFeCr-1
 ERNiMo-8
 ERNiCrMo-13
 ERNiCr-4
 ERNiCr-3
 ERNi-1
 Haynes-25
 Hayness-188
 MP35N
 Refractory 26
 Waspaloy alloy
 17-4PH
 17-7PH
 904L
 Nitronic 50
 Nitronic 60
 AL-6XN
 F55
 PH 13-8
 Haynes-230
 Nickel 200
 Sheet & Plate
 Strip & Foil
 Bar & Rod
 Pipe & Tube
 Bolts & Fasteners
 Flange & Ring
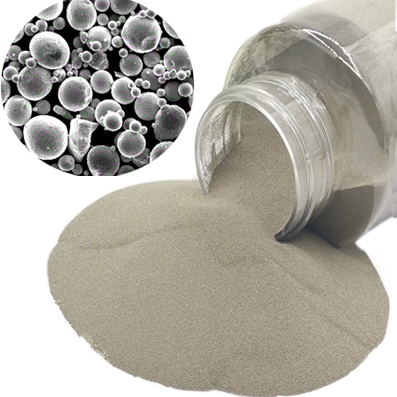 Nickel Alloy Powder


ERNiCrMo-1 vs ERNiCrMo-3: Advantages and Applications
1. Introduction
ERNiCrMo-1 and ERNiCrMo-3 are nickel-based welding filler metals classified under AWS A5.14. Both are designed for demanding welding applications involving nickel-chromium-molybdenum alloys, but their chemical compositions and performance characteristics are significantly different.
ERNiCrMo-1 corresponds to UNS N06007, while ERNiCrMo-3 corresponds to UNS N06625 (Alloy 625). ERNiCrMo-1 is particularly suitable when welding N06007-type nickel-chromium-molybdenum alloys, while ERNiCrMo-3 is widely selected for Alloy 625, Alloy 825, dissimilar-metal welding and corrosion-resistant applications.
2. Where ERNiCrMo-1 Has Advantages Over ERNiCrMo-3
2.1 Better Chemistry Matching for N06007-Type Alloys
The biggest advantage of ERNiCrMo-1 is material compatibility.
ERNiCrMo-1 is specifically associated with UNS N06007, while ERNiCrMo-3 is associated with UNS N06625.
When welding N06007-type nickel-chromium-molybdenum alloys, selecting a filler metal with a compatible chemistry can help engineers maintain the intended metallurgical characteristics of the welded joint.
Therefore, if the base metal is N06007 or a closely related alloy, ERNiCrMo-1 can be a more logical choice than ERNiCrMo-3.
2.2 More Balanced Alloying for Specific Ni-Cr-Mo Applications
ERNiCrMo-3 contains higher levels of molybdenum and Nb+Ta than ERNiCrMo-1. This is beneficial for many severe corrosion applications, but higher alloying is not automatically better for every application.
ERNiCrMo-1 provides a more moderate alloying balance that can be advantageous when the welding application does not require the higher alloy content of Alloy 625-type filler metal.
This can make ERNiCrMo-1 a practical choice for applications where corrosion resistance, metallurgical compatibility and economical alloy design are more important than maximizing alloy content.
2.3 Excellent Dissimilar-Metal Welding Capability
ERNiCrMo-1 can be considered for joining nickel-chromium-molybdenum alloys with steels and other nickel-based alloys.
This makes it useful for fabrication and repair work involving combinations of different materials. ERNiCrMo-3 also has excellent dissimilar-metal welding capability, so the advantage here is not that ERNiCrMo-1 is universally superior, but that it can provide an appropriate chemistry when the specific base-metal combination favors N06007-type filler metal.
2.4 Suitable for Corrosion-Resistant Cladding
ERNiCrMo-1 is suitable for applications where a nickel-based corrosion-resistant weld layer is required over a steel substrate.
Typical examples include:
- Pressure-vessel cladding
- Chemical-processing equipment
- Corrosion-resistant pipe components
- Repair welding
- Weld overlay applications
ERNiCrMo-3 is also widely used for nickel-alloy cladding, so ERNiCrMo-1's advantage is primarily its specific alloy chemistry and compatibility, rather than a universal superiority in corrosion resistance.
3. Applications of ERNiCrMo-1
ERNiCrMo-1 is particularly suitable for applications involving N06007-type nickel-chromium-molybdenum alloys and related fabrication requirements.
3.1. Chemical Processing Equipment
ERNiCrMo-1 can be used in the fabrication and repair of equipment exposed to corrosive chemical environments, including:
- Chemical reactors
- Process vessels
- Piping systems
- Heat exchangers
- Pumps and valves
- Corrosion-resistant components
3.2.Petrochemical Equipment
Its combination of nickel, chromium and molybdenum makes ERNiCrMo-1 suitable for selected petrochemical applications where resistance to corrosion and reliable welding performance are required.
3.3. Dissimilar-Metal Welding
ERNiCrMo-1 can be considered for joints involving:
- Nickel alloys to carbon steel
- Nickel alloys to stainless steel
- Nickel alloys to other nickel-based alloys
The exact filler-metal selection should be confirmed through the applicable WPS/PQR and service requirements.
3.4.Weld Overlay and Cladding
ERNiCrMo-1 is useful when a corrosion-resistant nickel-alloy surface is required on a steel component.
This approach can reduce the need to manufacture an entire component from an expensive nickel alloy while providing a corrosion-resistant surface in the service area.
3.5.Repair and Maintenance
ERNiCrMo-1 can also be considered for repair welding of nickel-chromium-molybdenum alloy components, particularly when the original base material is compatible with the filler-metal chemistry.
4. Where ERNiCrMo-3 Has Advantages Over ERNiCrMo-1
4.1 Higher Weld-Metal Strength
One of the key advantages of ERNiCrMo-3 is its high weld-metal strength. Reference data for ERNiCrMo-3 show a typical all-weld-metal tensile strength of about 114 ksi (approximately 785 MPa), with yield strength around 66 ksi and elongation around 35%.
The high strength comes largely from its Alloy 625-type Ni-Cr-Mo-Nb chemistry. Niobium and molybdenum contribute to solid-solution strengthening and the overall strength of the weld deposit.
This makes ERNiCrMo-3 particularly attractive for components exposed to both mechanical loading and corrosive environments.
4.2 Higher Molybdenum Content
ERNiCrMo-3 contains approximately 8–10% molybdenum. Molybdenum is especially important for improving resistance to localized corrosion, including pitting and crevice corrosion.
This is a major advantage in chloride-containing environments such as seawater, offshore facilities and chemical-processing systems.
4.3 Niobium Strengthening
ERNiCrMo-3 contains approximately 3.15–4.15% Nb + Ta. This is an important difference in its alloy design.
The combination of molybdenum and niobium helps produce a high-strength nickel alloy weld deposit while maintaining excellent corrosion resistance. This chemistry is one reason Alloy 625 and ERNiCrMo-3 are widely used in high-performance engineering applications.
4.4 Excellent Resistance to Pitting and Crevice Corrosion
ERNiCrMo-3 is particularly well suited to environments where chloride-induced corrosion is a concern.
Its combination of chromium and molybdenum provides strong resistance to general corrosion as well as localized corrosion. Research on ERNiCrMo-3 welded joints has also reported good corrosion performance in marine-related applications.
4.5 Excellent Dissimilar-Metal Welding Capability
Another important advantage is its versatility.
ERNiCrMo-3 can be used to join nickel alloys to:
- Carbon steel
- Low-alloy steel
- Stainless steel
- Super-austenitic stainless steel
- Other nickel-based alloys
It is also widely used for welding Alloy 625, Alloy 601, Alloy 825 and other high-alloy materials.
This makes ERNiCrMo-3 particularly useful when different material
5. Applications of ERNiCrMo-3
5.1 Oil and Gas Industry
ERNiCrMo-3 is widely used in oil and gas equipment where components can be exposed to chlorides, corrosive process fluids and demanding pressure conditions.
Typical applications include:
- Process piping
- Valves
- Pressure equipment
- Corrosion-resistant overlays
- Offshore production equipment
- Repair and maintenance welding
5.2 Offshore and Marine Engineering
Because of its excellent resistance to seawater-related corrosion, ERNiCrMo-3 is suitable for offshore structures and marine equipment.
Typical applications include subsea components, offshore piping, marine equipment and corrosion-resistant welded structures.
5.3 Chemical Processing
ERNiCrMo-3 is used for chemical-processing equipment where both corrosion resistance and mechanical reliability are required.
Applications include:
- Chemical process piping
- Heat exchangers
- Reactors
- Pressure vessels
- Storage tanks
- Corrosion-resistant weld overlays
5.4 Power Generation
ERNiCrMo-3 is also used in power-generation equipment, including piping systems and reactor-related components. Its combination of strength, oxidation resistance and corrosion resistance makes it suitable for demanding service environments.
5.5 Dissimilar-Metal Welding
One of the most commercially important applications is joining different materials.
ERNiCrMo-3 can be used for welding combinations involving nickel alloys, stainless steels, carbon steels and low-alloy steels. This makes it a valuable filler metal for equipment where thermal expansion, corrosion resistance and mechanical properties must be carefully balanced.
5.6 Cladding and Overlay Welding
ERNiCrMo-3 is also widely used to deposit a corrosion-resistant nickel alloy layer onto steel components.
This approach can provide a corrosion-resistant working surface while maintaining the structural strength and relatively lower cost of the steel substrate.
6. Conclusion
ERNiCrMo-1 and ERNiCrMo-3 are not simply “better” and “worse” versions of the same filler metal. They are designed for different alloy systems and applications.
The main advantages of ERNiCrMo-1 are its compatibility with UNS N06007-type Ni-Cr-Mo alloys, balanced alloy chemistry, good corrosion resistance, suitability for dissimilar-metal welding, and usefulness in corrosion-resistant cladding and repair applications.
ERNiCrMo-3, with its higher Mo and Nb+Ta content, offers excellent corrosion resistance and broad application versatility, particularly for Alloy 625 and related welding applications.
For N06007-type nickel alloys, chemical-processing equipment, dissimilar-metal joints, corrosion-resistant cladding and selected repair applications, ERNiCrMo-1 can be an excellent and technically appropriate choice.
The final filler-metal selection should always be confirmed according to the base-metal grade, WPS/PQR, operating conditions and applicable AWS/ASME requirements.
7.RFQ
7.1. RFQ – ERNiCrMo-3 vs ERNiCrMo-1
Q: What are the main differences between ERNiCrMo-1 and ERNiCrMo-3?
A: ERNiCrMo-1 is a Ni-Cr-Mo filler metal associated with UNS N06007, while ERNiCrMo-3 is associated with Alloy 625 / UNS N06625. ERNiCrMo-3 contains approximately 8–10% Mo and 3.15–4.15% Nb+Ta, giving it a high-strength and highly corrosion-resistant weld deposit.
7.2. RFQ – Which has better corrosion resistance?
Q: Which welding wire provides better resistance to pitting and crevice corrosion, ERNiCrMo-1 or ERNiCrMo-3?
A: ERNiCrMo-3 is generally the preferred choice for severe localized-corrosion environments. Its higher molybdenum content, combined with chromium and niobium, provides excellent resistance to pitting and crevice corrosion, particularly in chloride-containing environments.
7.3. RFQ – Strength of weld metal
Q: What are the typical mechanical properties of ERNiCrMo-3 weld metal?
A: ERNiCrMo-3 typically provides high-strength weld metal. A representative all-weld-metal value is about 760–790 MPa tensile strength, with approximately 35% elongation in the as-welded condition, depending on the welding procedure and test conditions.
7.4. RFQ – Applications
Q: Where is ERNiCrMo-3 commonly used?
A: ERNiCrMo-3 is widely used for welding Inconel 625, Inconel 601, Incoloy 825 and high-alloy stainless steels. It is also suitable for dissimilar-metal welding between nickel alloys, stainless steel, carbon steel and low-alloy steel.
7.5. RFQ – Which one should we choose?
Q: When should we choose ERNiCrMo-3 instead of ERNiCrMo-1?
A: Choose ERNiCrMo-3 when the project requires a combination of high weld-metal strength, excellent pitting and crevice corrosion resistance, chloride resistance and broad dissimilar-metal welding capability. However, the final selection should be based on the base-metal grade, service environment and qualified WPS/PQR requirements.
Contact Huiyu Alloys today for nickel alloy grade selection, material specifications, customized sizes, technical consultation, and quotation.
Website: https://www.huiyualloys.com/
Email: hyalloys@gmail.com sales6@huiyualloys.com
Whatsapp: (86 )17627989936
Huiyu Alloys — Your Reliable Nickel Alloy Manufacturer & Supplier in China.